Belt conveyor
Product Details
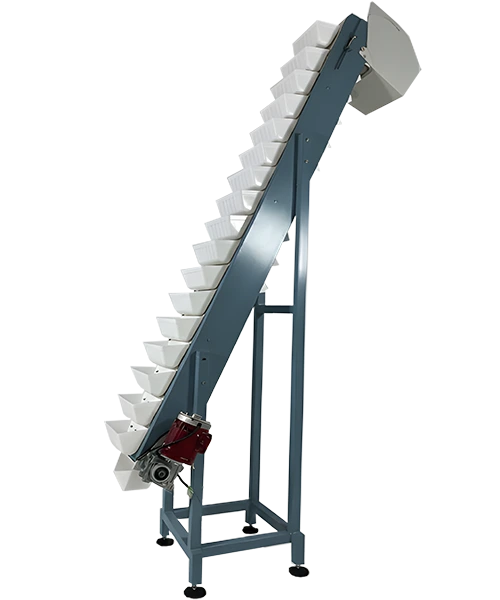
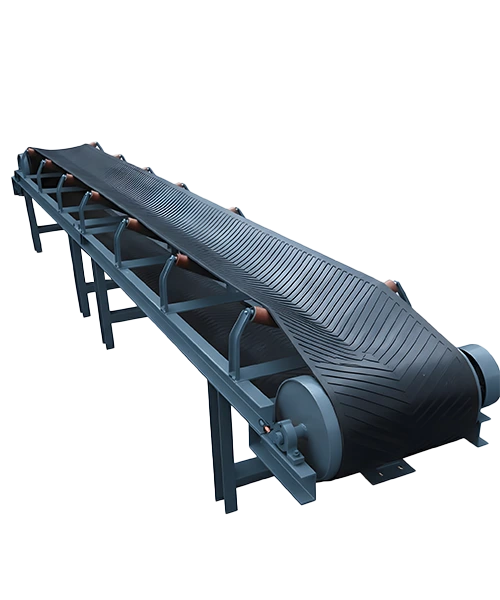
The Belt Conveyor manufactured by Shiv Shakti Fabrications is a reliable material handling system designed for smooth and continuous transportation of bulk materials in fertilizer plants and industrial production facilities. This heavy-duty conveyor system uses a moving belt supported by rollers to transfer materials efficiently between different stages of the production process.
Our Belt Conveyor is engineered to provide stable and efficient material movement across long distances within production plants. As the belt moves over the rollers, materials such as fertilizer granules, mineral powders, and bulk solids are transported safely from one processing machine to another. This simple yet effective mechanism helps maintain a continuous workflow and improves overall production efficiency.
One of the main advantages of the belt conveyor system is its ability to handle large volumes of materials with minimal energy consumption. The conveyor belt moves smoothly over the support rollers while maintaining stable material flow, making it ideal for industries where continuous transportation of bulk materials is required. Because of this efficiency, the Belt Conveyor is widely used in fertilizer production plants, mineral processing industries, and bulk material handling operations.
The machine structure is fabricated using strong industrial steel components designed to withstand heavy loads and long working hours. The durable frame supports stable belt movement while the drive mechanism ensures consistent conveyor speed. This robust construction allows the Belt Conveyor to operate reliably in demanding industrial environments with minimal maintenance requirements.
Efficient material transportation is a critical part of fertilizer production systems. By automating the movement of raw materials and finished granules, the Belt Conveyor helps reduce manual labor, improve production speed, and maintain smooth workflow between different processing stages in the manufacturing line.
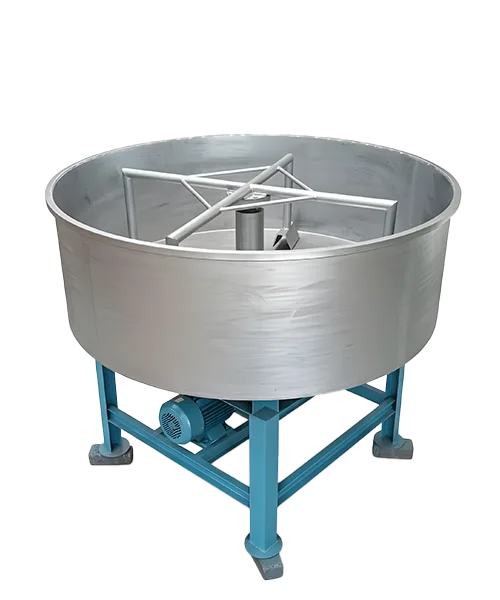
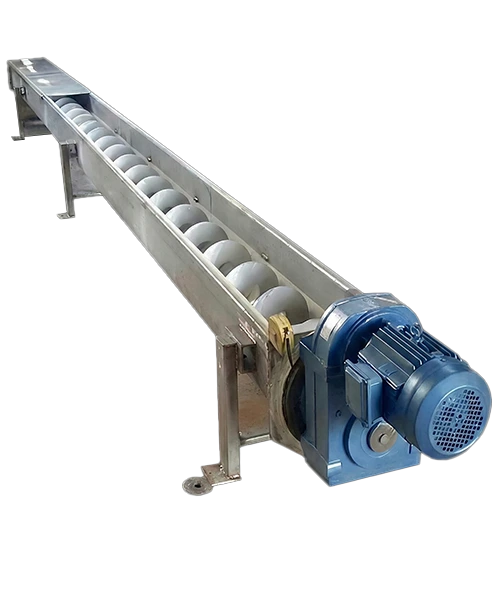
In modern fertilizer production plants, the Belt Conveyor is commonly used together with machines such as the Pan Disc Granulator Set for granule formation, the Pan Mixer Machine for proper mixing of raw materials, and the Screw Conveyor Hopper for controlled feeding and transfer of powder materials during production.
Why Choose Shiv Shakti Fabrications
At Shiv Shakti Fabrications, we manufacture industrial fertilizer machinery with strong fabrication quality and practical engineering designed for real industrial environments. Our machines are built to deliver reliable performance, efficient material handling, and long operational life, helping fertilizer manufacturers maintain consistent production and high-quality output.
With its efficient material transport mechanism, durable industrial construction, and ability to handle continuous production flow, the Belt Conveyor remains an essential machine for fertilizer plants and bulk material handling industries.